skip to Main Content
Choosing the 2026 best Copper Part Machining manufacturers requires more than comparing glossy websites. It demands evidence from the shop floor. Buyers should examine machining tolerances, copper grades, production capacity, inspection methods, and delivery records. A strong supplier should explain how it controls burrs, heat, tool wear, and surface damage during CNC milling or turning. Ask for sample reports. Review actual parts.
Dr. David A. Stephenson, a respected metal-cutting researcher and author, stated, “The cutting tool and the workpiece are partners in the machining process.” This principle remains highly relevant for copper components. Copper conducts heat quickly, deforms easily, and can smear across an unsuitable cutting edge. Skilled manufacturers therefore select sharp carbide tools, stable fixtures, suitable feeds, and controlled lubrication. They also monitor dimensions after cooling. Small details matter.
The best manufacturers combine technical experience with dependable communication. They should support prototypes, repeat orders, and design adjustments without creating confusion. Certifications can help, but certificates alone do not prove consistent workmanship. Request traceability documents, inspection data, and references from comparable projects. Look for suppliers serving electrical, medical, aerospace, and industrial applications. Their experience reveals practical competence.
No ranking is flawless. A manufacturer that excels at prototypes may struggle with high-volume production. Another may offer excellent tolerances but weaker logistics. This guide compares those differences carefully. It considers measurable performance, not advertising language. Copper Part Machining is a specialized process. The right partner should understand both the material and the consequences of every machining decision.
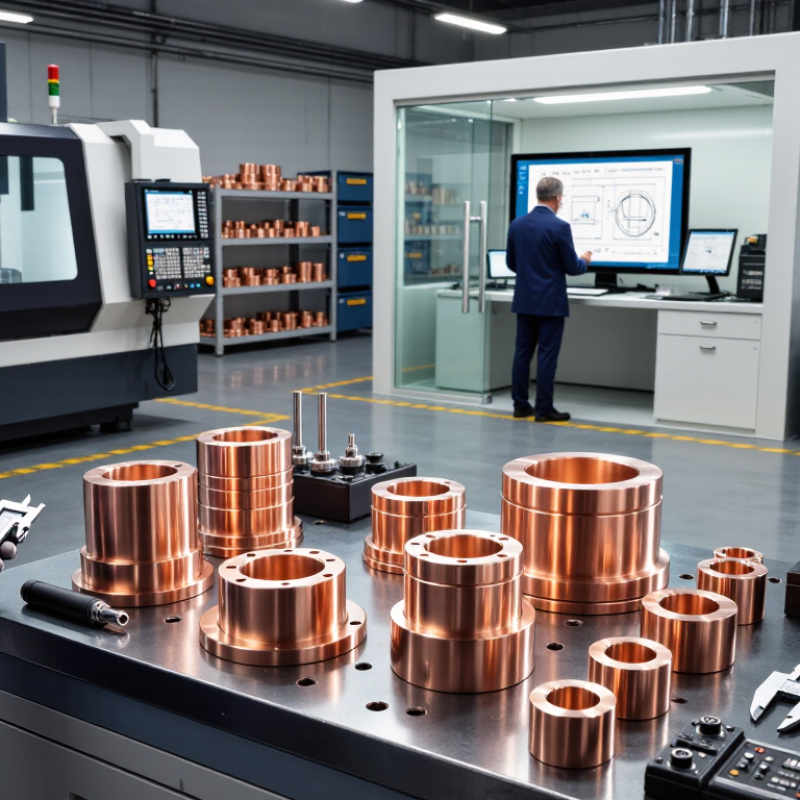
A leading copper part machining manufacturer in 2026 does more than cut metal accurately. It understands copper’s high conductivity, softness, and tendency to create burrs during machining. Experienced engineers select suitable tooling, cutting speeds, and coolant methods for each alloy and geometry. They also review drawings before production begins. Small misunderstandings can become expensive defects.
Reliable manufacturers control every stage, from raw material certification to final inspection. They may use coordinate measuring machines, surface-finish checks, and documented process records. Traceability matters when a copper connector must perform consistently in heat, vibration, or electrical assemblies. Clear communication is equally important. A trustworthy supplier reports risks early instead of hiding delays. No workshop is perfect. Even strong processes need review when thin walls distort or edges smear.
Tips: Ask how the supplier manages burrs, verifies conductivity, and protects soft surfaces during handling. Request sample inspection data, material certificates, and realistic tolerance guidance. Judge the response, not only the quoted price. A vague answer may signal weak process control.
Practical experience should guide design feedback. For example, a deep narrow pocket may be machinable but costly and unstable. A skilled manufacturer suggests a small radius, better clamping access, or a more suitable tolerance. That advice shows engineering judgment rather than simple production capacity. Dependable service also includes secure documentation, repeatable scheduling, and inspection results that match the agreed specification.
Selecting a copper machining manufacturer requires more than checking equipment lists. The USGS Mineral Commodity Summaries 2025 estimated global copper mine production at about 22 million metric tons in 2024. This scale highlights copper’s industrial importance, but it does not prove machining quality. Experienced buyers should examine material traceability, alloy control, and process stability. Ask for mill certificates, conductivity results, and documented inspection methods. Small details matter.
Copper transfers heat quickly and can smear during cutting. A capable shop should explain tool geometry, cutting speeds, coolant control, and burr prevention. Review sample parts under magnification. Look for torn edges, embedded chips, and uneven pockets. Critical dimensions need coordinate measuring machine reports, not visual approval alone. Capability studies, including Cp and Cpk values, can reveal whether a process remains stable across production runs.
The International Energy Agency’s Global Critical Minerals Outlook 2024 identifies copper as essential to expanding electricity networks and clean-energy systems. Demand pressure may increase the need for reliable precision components. Still, a high-volume claim deserves evidence. Check first-article reports, nonconformance records, and corrective-action history. Delivery performance also matters, especially for copper parts used in thermal systems or electrical assemblies. Perfect consistency is difficult. I would challenge any supplier promising zero variation without showing real process data.
Choosing the 2026 best copper part machining manufacturer requires more than comparing prices. Quality begins with verified material control. Ask for mill certificates, alloy identification, and full batch traceability. Common materials include C110 copper and copper alloys with different conductivity, hardness, and machinability. A capable manufacturer should explain these differences clearly.
Certification supports trust, but it is not proof of perfect production. ISO 9001 shows structured quality management, while ISO 13485 may suit medical applications. Confirm whether certificates are current and relevant to your project. Review inspection records, calibration dates, and first-article reports. For tight components, request CMM measurements, thread checks, burr inspection, and surface-finish data. Production criteria also matter. Look for stable CNC capacity, controlled coolant, suitable tooling, and documented process control. A supplier may promise excellent accuracy, yet actual samples can reveal tool marks or inconsistent edges. I have learned that factory visits and sample reviews often expose small weaknesses early.
Tips: Request three sample parts from one production batch. Measure critical diameters independently. Ask how rejected parts are contained and corrected. Check realistic lead times, not optimistic quotations. Clarify packaging, corrosion protection, and inspection responsibilities. Certifications can expire, and even experienced teams sometimes overlook a minor drawing note. That detail may become a costly production issue.
| Evaluation Dimension | Recommended Benchmark | Technical Relevance to Copper Parts | Evidence to Request | Priority |
|---|---|---|---|---|
| Quality Management | ISO 9001-certified quality management system | Provides a structured process for document control, inspection, corrective action, traceability, and continual improvement. | Current certificate, certification scope, issuing body, and expiration date | Essential |
| Material Traceability | Heat-lot or batch-level traceability from raw material to finished part | Copper conductivity, hardness, alloy composition, and machinability can vary by grade and supply condition. | Mill certificates, material certificates, lot identification, and receiving inspection records | Essential |
| Copper Material Range | Documented capability for commercially relevant copper and copper-alloy grades | Common applications may require high-conductivity copper, free-machining copper, brass, bronze, or precipitation-hardened alloys. | Approved material list, grade cross-reference, and sample certificates | Essential |
| Dimensional Accuracy | Typical CNC tolerance capability of ±0.01 mm to ±0.05 mm, depending on feature size and design | Copper is relatively soft and thermally conductive, so tool deflection, burr formation, and heat management affect dimensional stability. | Inspection reports, capability studies, GD&T examples, and equipment specifications | Essential |
| Surface Finish | Ra 0.8–3.2 µm for many precision-machined surfaces, subject to drawing requirements | Surface finish influences electrical contact resistance, sealing performance, appearance, and coating adhesion. | Surface roughness reports, profilometer records, and representative sample results | High |
| Machine Capability | Multi-axis CNC milling and turning with documented work-envelope limits | Complex connectors, busbars, terminals, heat-transfer components, and threaded parts may require simultaneous or indexed multi-axis machining. | Machine list, axis configuration, maximum workpiece size, spindle range, and demonstrated parts | High |
| Process Control | Approved work instructions, first-article inspection, in-process checks, and final inspection | Controlled processes reduce variation in hole position, thread quality, flatness, burr condition, and critical electrical-contact features. | Control plans, inspection plans, first-article reports, and process flow diagrams | Essential |
| Measurement System | Calibrated CMM, optical measurement, height gauges, micrometers, and surface-finish equipment | Accurate measurement is required for tight positional tolerances, profile requirements, concentricity, and small copper features. | Calibration records traceable to recognized national or international standards | Essential |
| Electrical Performance | Material and conductivity verification when electrical performance is specified | Electrical components may require confirmation of alloy, conductivity, plating condition, contact resistance, or current-carrying performance. | Conductivity test results, alloy verification, coating records, and customer-specific test reports | Application-Based |
| Burr and Cleanliness Control | Defined deburring, chip removal, washing, drying, and packaging procedures | Copper burrs and chips can interfere with electrical contacts, fluid passages, seals, threads, and assembly operations. | Deburring standard, cleanliness specification, particle-control method, and inspection photographs | High |
| Surface Treatment | Controlled capability for plating, passivation, tinning, nickel treatment, or protective finishing where required | Finishes may improve corrosion resistance, solderability, wear resistance, appearance, or compatibility with mating materials. | Process specifications, coating thickness reports, adhesion tests, and external processor approvals | Application-Based |
| Environmental Compliance | Material and process controls aligned with applicable restricted-substance requirements | Electrical and electronic applications may require controlled levels of restricted substances and documented supplier declarations. | Compliance declarations, supplier material statements, and laboratory test reports when necessary | High |
| Production Capacity | Capacity plan covering prototype, low-volume, and repeat production requirements | Stable capacity helps prevent delivery delays caused by machine loading, tooling shortages, inspection bottlenecks, or material lead times. | Capacity statement, production schedule, equipment utilization, and documented lead-time assumptions | High |
| Tooling and Programming | Controlled CNC programming, tool-life monitoring, and documented setup repeatability | Copper machining often benefits from sharp tooling, suitable rake geometry, controlled feeds and speeds, and reliable chip evacuation. | Tooling standards, setup sheets, tool-life records, and sample process documentation | High |
| Delivery Performance | Measured on-time delivery performance with formal corrective action for delays | Consistent delivery is important for electrical assemblies, industrial equipment, thermal systems, and other scheduled production programs. | Anonymized delivery KPI data, order review procedure, and escalation process | High |
| Industry-Specific Certification | Additional certification matched to the end-use sector when required | Medical, automotive, aerospace, and other regulated applications may require sector-specific controls beyond general quality certification. | Relevant certificate, scope, audit status, and evidence that the scope covers the required manufacturing process | Application-Based |
| Engineering Support | Design-for-manufacturing review before production approval | Early review can identify thin walls, deep cavities, difficult internal corners, burr-sensitive features, and unnecessary tight tolerances. | DFM checklist, technical review workflow, drawing-markup examples, and engineering response times | High |
| Supply-Chain Risk | Qualified sources for copper materials, tooling, finishing, and critical subcontracted operations | Material availability and outsourced finishing can affect cost, continuity, lead time, and compliance documentation. | Approved supplier procedure, dual-source strategy, risk assessment, and business-continuity plan | High |
Note: Benchmarks are general procurement guidance. Final acceptance criteria should be defined by the engineering drawing, applicable material specification, end-use regulations, and validated production requirements.
Comparing manufacturers starts with the copper grade, not the quotation. C101 oxygen-free copper suits high-conductivity parts, while C110 works well for many busbars and electrical fittings. Copper conducts heat quickly and can smear during cutting. Ask about cutting tools, chip control, coolant selection, and heat distortion. A supplier experienced with heat sinks may not be equally capable with thin connectors or precision electrodes.
The International Copper Study Group’s 2024 market outlook projected refined copper usage above 26 million metric tons in 2025. This scale increases pressure on material traceability and delivery planning. The USGS Mineral Commodity Summaries 2025 reported global mine production near 23 million metric tons for 2024. These figures do not prove machining quality, but they underline the need to verify material sources and supply resilience.
Request inspection samples for each component family. Check flatness on busbars, burr height on connectors, hole position on cooling plates, and surface finish on sealing faces.
Review Cpk data, calibration records, first-article reports, and nonconformance handling. ISO 9001 certification helps, but it is not enough by itself. Ask for actual measurement records.
Keep the test practical. Use the same drawing, tolerance, and batch size. Compare cycle time, scrap rate, packaging, and corrective-action speed. A low unit price can hide unstable processes. I have seen seemingly minor burrs interfere with assembly. The mistake is trusting a polished capability sheet too quickly. Run a small pilot order, then reassess.
A reliable copper machining partner should understand more than basic CNC programming. Ask which copper grades they routinely process, including pure copper, brass, and bronze. Their answer should match your electrical, thermal, and mechanical requirements. Experience matters here. Copper can smear, deform, and create sharp burrs when cutting conditions are poorly controlled.
Request a sample inspection report before approving production. Check dimensional results, surface finish, burr control, and thread quality. Ask how they verify tight tolerances on thin walls or deep holes. A coordinate measuring machine, calibrated gauges, and documented inspection records show stronger process discipline. Also review material certificates and heat-lot traceability. Small details can prevent expensive confusion later.
Discuss tooling, coolant selection, workholding, and production capacity. Copper parts may require sharp tools, stable clamping, and careful heat management. Ask for a design-for-machining review with clear suggestions, not vague promises. A capable supplier should explain risks before quoting.
ISO-based quality procedures can support consistency, but certificates alone prove little. Visit the facility if practical. Look at actual work areas, inspection equipment, and finished parts. A low price is tempting. It can hide weak process control. No checklist is perfect. I have seen technically strong suppliers miss delivery expectations because communication was overlooked. Confirm response times, corrective-action procedures, packaging, and realistic lead times before signing the purchase order.
